Ensuring Consistent Quality Control in Bulk Insulated Bottle Manufacturing
At Youke Flask, delivering premium insulated bottles in bulk without compromising quality is at the heart of our manufacturing philosophy. Consistent quality control isn’t just a process—it’s a commitment to our customers, ensuring every thermal flask meets rigorous standards for performance, safety, and durability. In this blog, we’ll walk you through the multi-layered strategies we employ to maintain excellence throughout the bulk production of insulated bottles.
1. Rigorous Incoming Material Inspection (IQC)
The foundation of quality begins with raw materials. Our Incoming Quality Control (IQC) team thoroughly assesses every component—from food - grade stainless steel (for vacuum layers) and BPA - free plastics to silicone seals and paint coatings. We:
- Verify material certifications (e.g., FDA - approved plastics, LFGB - compliant stainless steel) to ensure safety and compliance.
- Conduct supplier audits and maintain a strict approval process for new vendors.
- Perform sampling inspections for dimensional accuracy, material purity, and aesthetic quality (e.g., scratch - free stainless steel sheets).
2. In - Process Quality Monitoring (IPQC)
During production, our In - Process Quality Control (IPQC) team oversees every stage—from bottle forming and welding to powder coating and assembly. Key actions include:
- Automated vision systems detect surface defects (e.g., dents, uneven welds) in real time.
- Manual inspections at critical checkpoints (e.g., after welding, before insulation) to catch human error or equipment drift.
- Data logging of process parameters (e.g., temperature in the vacuum sealing chamber) to ensure repeatability and traceability.
3. Comprehensive Final Quality Checks (FQC)
Before packaging, every batch undergoes Final Quality Control (FQC) with a focus on performance, safety, and aesthetics:
- Insulation Testing: We simulate real - world use by testing temperature retention (e.g., 95°C water after 24 hours, 5°C ice water after 24 hours) against internal and industry standards.
- Leak & Seal Testing: Bottles are pressure - tested or inverted to ensure 100% leak - proof performance (critical for both hot and cold liquids).
- Durability Testing: Random samples undergo drop tests (mimicking shipping impacts) and cycle tests (opening/closing lids 5,000 + times) to ensure long - term reliability.
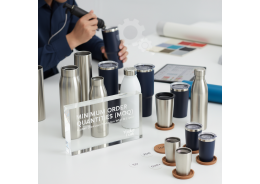
- Aesthetic Audits: Trained inspectors check for color uniformity, smooth finishes, and logo accuracy using AQL (Acceptable Quality Limit) 2.5 sampling plans.
4. Specialized Testing Laboratories
Our in - house lab is equipped to validate key performance metrics:
- Thermal Performance: Climate - controlled chambers simulate extreme temperatures to test insulation efficiency.
- Chemical Safety: We test for heavy metals (e.g., lead, cadmium) and ensure materials meet FDA, LFGB, and EU food - contact regulations.
- Structural Integrity: Tensile and compression tests verify lid strength, handle durability, and overall product robustness.
5. Employee Training & Empowerment
Quality is a team effort. We invest in:
- Regular training on quality standards (ISO 9001, industry best practices) and advanced inspection techniques.
- Empowering operators to stop production if a quality issue is detected (via our “quality first” culture).
- Cross - training teams to ensure flexibility and shared accountability across production stages.
6. Equipment Maintenance & Calibration
High - precision machinery (e.g., laser welders, vacuum sealers) requires strict upkeep:
- Preventive maintenance schedules to minimize downtime and equipment - related defects.
- Calibration of testing instruments (e.g., thermometers, pressure gauges) against national standards to ensure accuracy.
7. Compliance & Certifications
We adhere to global standards to ensure market access and trust:
- Certifications: ISO 9001 (quality management), FDA (US food safety), CE (EU safety), and BSCI (ethical manufacturing).
- Regular audits by third - party agencies to validate our processes and products.
8. Customer Feedback & Continuous Improvement
Post - delivery, we analyze customer feedback (e.g., reviews, warranty claims) to identify areas for improvement. This feedback loop drives:
- Root - cause analysis of issues (e.g., lid leakage, paint chipping) to update production protocols.
- Design iterations (e.g., improved lid ergonomics, enhanced insulation layers) based on real - world use data.
Conclusion
At Youke Flask, quality control in bulk manufacturing is a dynamic, data - driven journey. By combining strict inspections, advanced testing, employee ownership, and customer - centric improvements, we ensure every insulated bottle meets the high standards our brand—and your business—demands. Whether you’re a retailer, distributor, or brand partner, you can trust our commitment to consistent quality, batch after batch.

 English
 German
 French
 Russian
 Spanish
 Japanese
 Korean
 Portuguese
 Ukrainian
 Arabic
 Italian